CZ Purlin Roll Forming Machine
CZ Purlin Roll Forming Machine
One line, two sections: C and Z purlin from 80–350 mm web and up to 5 mm steel, with a C-to-Z section change measured in minutes rather than hours. Prepunching and precutting heads mean a size change is entered on the touch screen, not made with a spanner.
- Sheet thickness 1.5–5.0 mm
- Forming stations 20–24
- Main motor 15 kW
- Line speed 12–25 m/min
Applications & material
What this machine is built to produce
The same frame serves different buyers depending on the profile and the material grade. Start from the application closest to your project, then check the section sizes below.
Where it is used
- Portal frame purlins where the roof needs C sections and the lapped Z runs need Z sections.
- Fabricators who quote both purlin types and cannot justify two dedicated lines.
- Plants producing infinite sizes within the machine range without changing rollers.
Suitable material
- Hot-dip galvanised steel
- 1.5–5.0 mm
- Cold-rolled mild steel
- 1.5–5.0 mm
- High-strength steel (S350 / S450)
- 1.5–4.0 mm
- Prepainted steel
- 1.5–3.0 mm
Target profiles
- C purlin, web 80–350 mm
- Z purlin, web 80–350 mm, lapped flange
- C and U channel without changing rolls
- Any size within the range, set from the touch screen
Not on the list? The rolls are cut to a drawing — send yours and we will confirm feasibility.
Technical data
CZ Purlin Roll Forming Machine specifications
Values below are for the standard build of this model. Thickness range, station count and motor rating are re-calculated when the profile or the steel grade changes.
Send your profile drawing| Parameter | Value |
|---|---|
| Web height | 80–350 mm (100–300 mm typical) |
| Sheet thickness | 1.5–5.0 mm (3.0 mm for full-speed production) |
| Forming stations | 20–24 |
| C / Z changeover | about 1 minute for the section switch |
| Size change | 1–2 minutes on the screen; add 20–40 minutes if web height changes |
| Decoiler | 3 t manual, coil ID 508 ± 30 mm, OD 1800 mm |
| Leveling | 5 rollers (2 up, 3 down), Cr12 guide rollers HRC 58–62 |
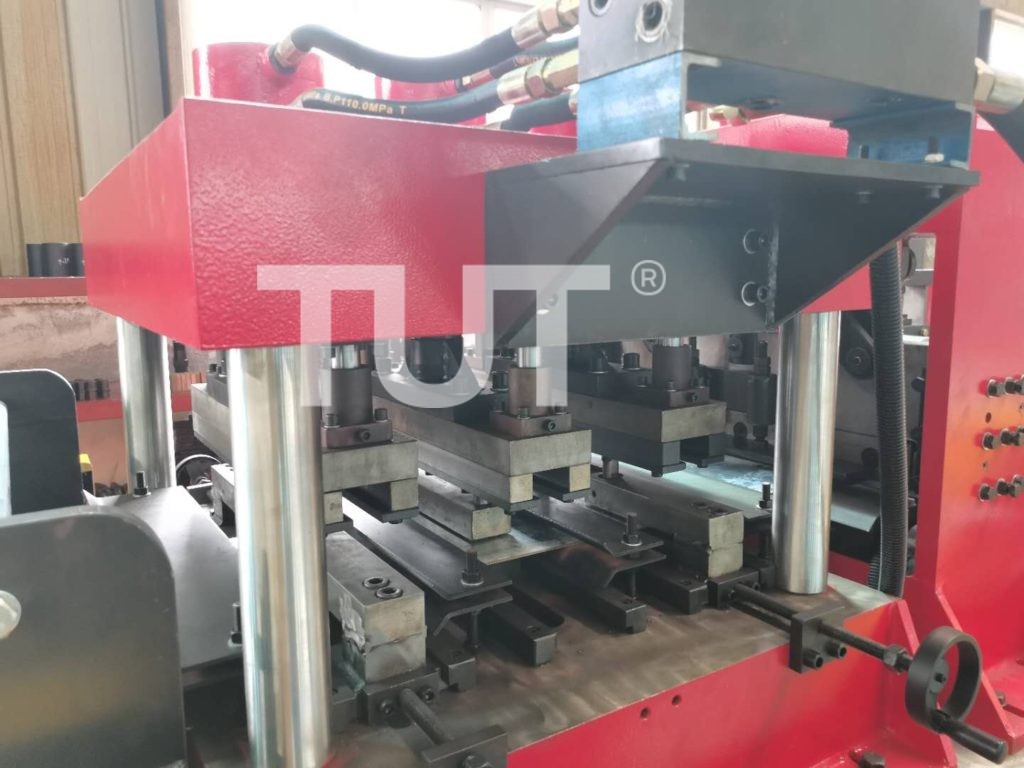
| Hydraulic punch | 3 punch mould sets, Cr12MoV |
| Hydraulic cutting | Cutting width ≤500 mm, blade Cr12, HRC 58–62 |
| Shaft | 40Cr, φ80 mm, HB 250–280 |
| Roller material | GCr15, HRC 58–62, chrome plated |
| Main motor | 15 kW |
| Hydraulic station | 7.5 kW |
| Control | Panasonic PLC + MCGS touch screen |
| Bearing | Harbin 6213Z / 6212Z |
Web height and thickness are frame limits: continuous production is normally run at 100–300 mm and up to 3.0 mm, with the upper figures used for short runs and heavy sections.
Working process
From coil to finished profile
The sequence below is the standard layout for this model. Stations are added or removed when the section needs more forming passes.
- 01 Decoiling 3 t manual decoiler, coil ID 508 ± 30 mm, OD up to 1800 mm.
- 02 Feeding & leveling 5-roller leveler (2 up, 3 down) with Cr12 guide rollers.
- 03 Hydraulic punching Three punch mould sets for web and flange holes, positioned by the control.
- 04 Hydraulic cutting Pre-cut before forming, so the cut is square and no blade change is needed for a size change.
- 05 Main roll forming Forming with rails and hand wheels for web height and thickness; C/Z changeover by a one-minute switch.
- 06 Run-out Finished purlin leaves on the outfeed table.
Main components
- 3 t manual decoiler Coil ID 508 ± 30 mm, OD 1800 mm, manual expansion.
- Feeding and leveling unit 5 rollers (2 up, 3 down), Cr12 guide rollers HRC 58–62.
- Hydraulic punch Three punch mould sets in Cr12MoV; holes anywhere on the web and flange.
- Hydraulic cutting Pre-cut, width ≤500 mm, Cr12 blade HRC 58–62.
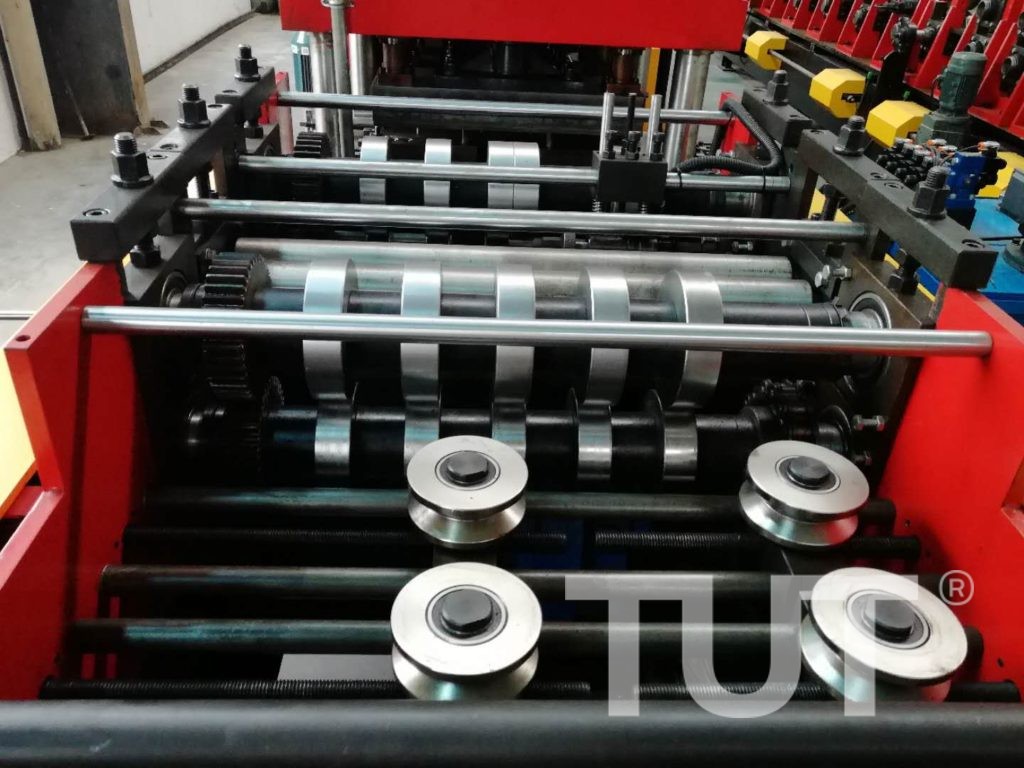
- Main roll forming part GCr15 rolls HRC 58–62 chrome plated, 40Cr φ80 mm shafts, guide-rail size adjustment with hand wheels.
- PLC control box Panasonic PLC, MCGS touch screen; enter part number, dimensions and quantity.
- Hydraulic station 7.5 kW pump unit.
- Transmission Speed reducer, coupling, transmission shaft, bevel gear, high-strength screw and guide rails.
Optional configuration
Samples & running line
Profiles from this machine, and the line in motion
Every line is sampled before shipment. Photos below are from the build of this model; the video shows the line running on production material.
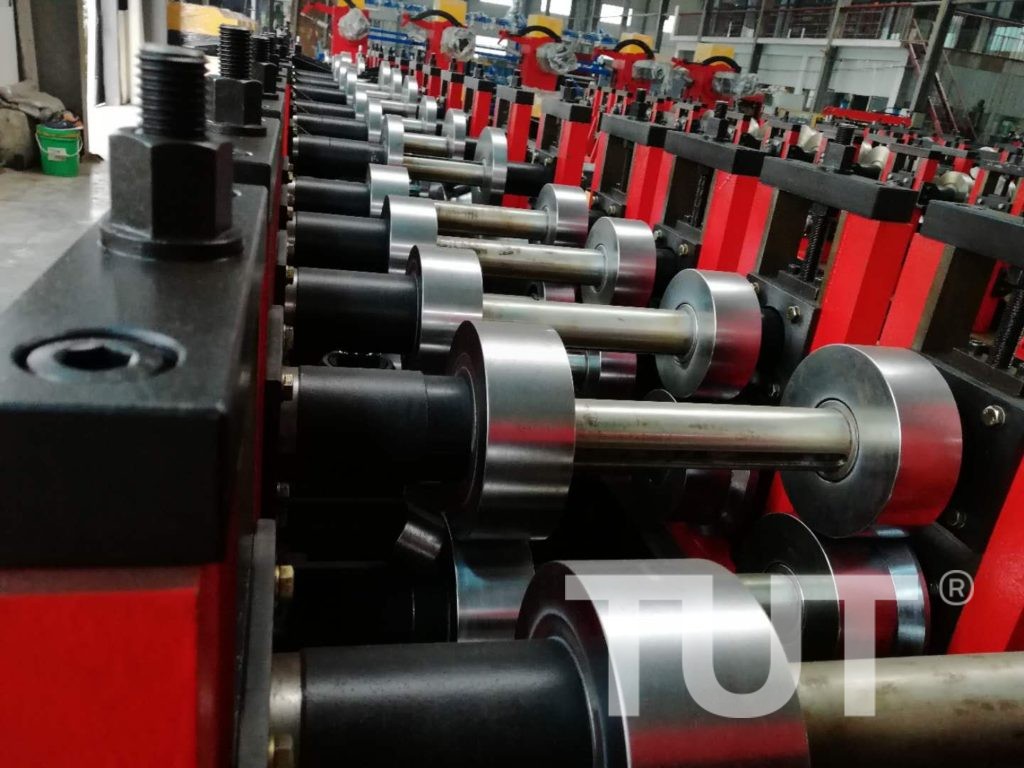
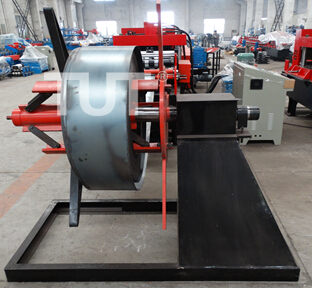
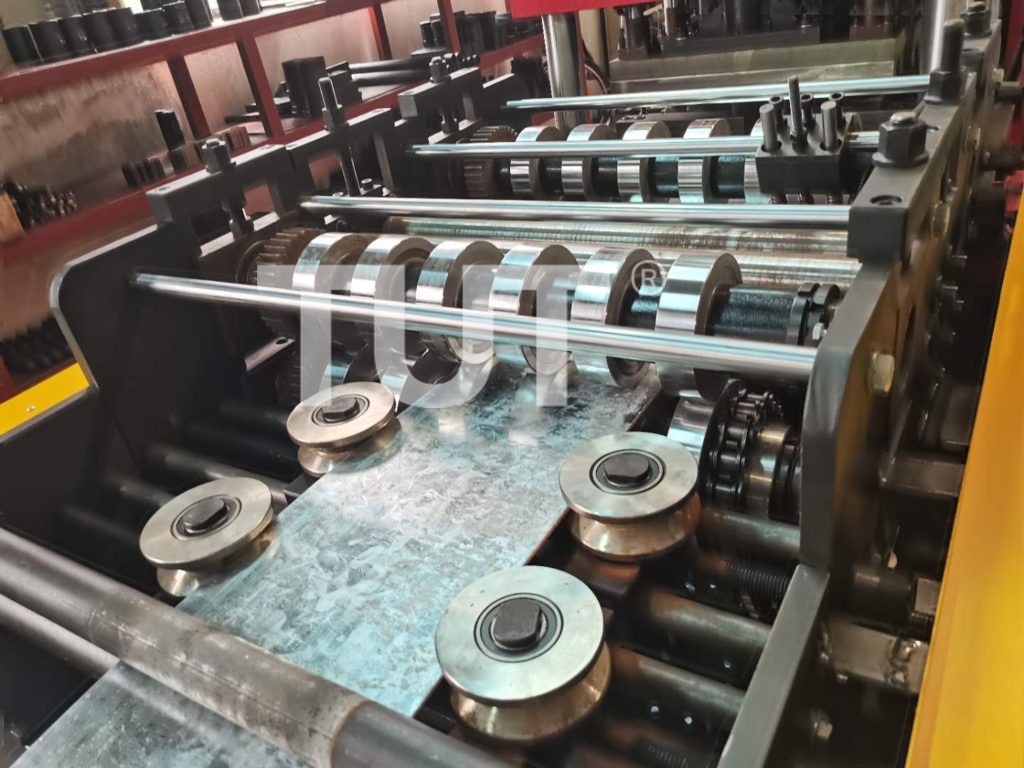
Samples are supplied in both C and Z from the same coil, at the minimum and maximum web height, so you can verify the changeover and the lap fit.
Video on request
Ask for the latest running video
We record a fresh clip of this model before shipment. Ask for it and we will send the current video, plus a live call from the factory floor if you want to see the line under power.
Profile range
- C purlin, web 80–350 mm
- Z purlin, web 80–350 mm, lapped flange
- C and U channel without changing rolls
- Any size within the range, set from the touch screen
Engineering & service
Custom build, installation and after-sales
A roll forming line is only finished when it runs on your material at your output. These three parts of the scope are quoted together with the machine.
Custom engineering
The value of this line is that a purlin size is a number on a screen, not a roll change. If your order book is mostly one or two sizes, a dedicated C line runs faster; if it is a mix of C and Z widths every week, this is the machine that keeps the changeover off the critical path.
- Tooling cut to your drawing or sample
- Electrics to your plant voltage and frequency
- Layout and foundation drawing before shipment
Installation & training
An engineer supervises installation and trains your operators on the actual line — not on a generic manual. Training covers coil loading, size change, tooling change and daily maintenance.
- On-site commissioning and first production run
- Operator training on your material
- Remote video support if travel is not practical
After-sales support
A 12-month warranty on the mechanical parts, with a 24-hour response on technical enquiries. Wearing parts — rollers, punch dies, hydraulic seals — are kept in stock for fast dispatch.
- 12-month mechanical warranty
- Spare rollers and dies from stock
- 24-hour response on remote support
What we need from you
Four inputs that decide 80% of the design
- 01 Profile drawing with dimensions and tolerances
- 02 Material type, thickness range and steel grade
- 03 Target output per shift or per day
- 04 Plant voltage, frequency and available floor length
Customer cases
This machine in production
Delivery records for this machine family — the country it went to, the section it produces and the year it shipped. Each project page carries the order specification and the factory test run.
FAQ
Questions buyers ask about this machine
Answers come from real quotation discussions on this model. If your question is not here, ask it in the form below and an engineer will answer it directly.
How long does it take to change from C to Z purlin?
The section switch takes about one minute — the entry guide flips and the idle hand is disengaged, no rollers are removed. If the web height also changes, allow 20–40 minutes for the reset and a trial length check, which is the figure that matters when you cost a small mixed order.
Can it punch holes anywhere on the purlin?
Yes, on the web and both flanges, using three punch mould sets. Hole positions are entered in the control, and the optional servo size adjustment keeps them accurate when the section changes.
What is the maximum thickness?
The frame handles up to 5 mm, but full-speed production is realistic up to 3 mm. Above 3 mm the line runs slower and the cut quality needs checking on high-strength grades.
Why pre-cut instead of post-cut?
Pre-cutting means the blade does not have to match each section size, so a size change needs no blade change. It also keeps the cut square on thick material.
What is the delivery time?
60–85 days after approval, depending on the punch layouts and whether a decoiler upgrade is included.
Related equipment
Other machines in this range
C Purlin Roll Forming Machine
C purlin roll forming machines producing C and U channel sections from 1.5–5.0 mm steel, with in-line punching and hydraulic…
View Details
Deck Floor Roll Forming Machine
Deck Floor Roll Forming Machine is designed to produce various types of metal decks, which is the preferred method of…
View Details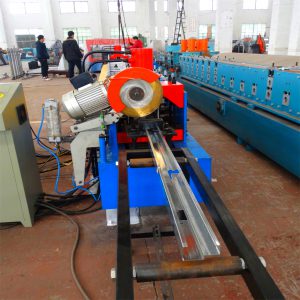
Door Frame Roll Forming Machine
Door Frame Roll Forming Machine is designed to produce steel metal door frame which are widely used for commercial, institutional,…
View DetailsRequest a quotation
Tell us the profile, we will configure the line
Send the drawing, the material and the output you need. You get a line configuration, tooling scope and delivery schedule — usually within one working day.
- Reply within one working day
- Quotation itemised by machine, tooling and options
- Engineering review of your profile before pricing