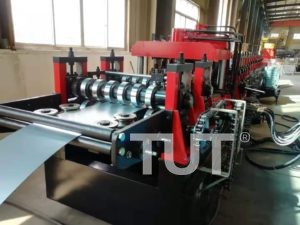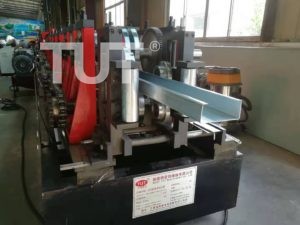
C Purlin Roll Forming Machine
C purlin roll forming machines producing C and U channel sections from 1.5–5.0 mm steel, with in-line punching and hydraulic cutting. Factory direct.
View DetailsRoll forming lines
Lines for C, Z and CZ steel purlins in 1.5–5.0 mm high strength coil, with in-line punching, web height adjustment and the changeover speed that decides output per shift.
C purlin roll forming machines producing C and U channel sections from 1.5–5.0 mm steel, with in-line punching and hydraulic cutting. Factory direct.
View DetailsC Z Purlin Roll Forming Machine is used to produce C Purlin and Z Purlins with very less changeover time that the exchange time…
View DetailsTechnical overview
A purlin order is a mix of web heights, flange widths and hole patterns. A line that runs 25 m/min but needs a full day to change size earns less than one that runs 15 m/min and changes over in an hour.
The family splits three ways. C purlin lines form a channel with equal or unequal flanges; Z purlin lines form the nested Z that laps at the purlin line and needs a dedicated tooling set for the opposite hand; CZ lines combine both on one frame with a switching device at the entry, which is the usual choice when a plant sells both types.
Web height is changed either by moving the side units on linear guides with the shaft line kept in mesh, or by cassette exchange. In-line 3-side punching handles flange holes, web holes and the sleeve holes at the lap, positioned by servo so hole patterns follow the cut length. Cutting is a hydraulic post-cut shear sized to the section thickness. For the buildings these purlins carry, see building and construction.
Figures are typical for this category. Final values follow the profile drawing and material grade.
Discuss your specificationApplications
The same machine serves different industries depending on the profile, coating and output. Start from the application closest to your project.
FAQ
Answers come from real quotation discussions. If your question is not here, ask it directly and an engineer will answer.
If more than a third of your orders are Z purlin, a CZ line usually pays back within a year because the changeover is minutes rather than a shift. If you sell almost only C purlin, a dedicated C line is cheaper and runs faster.
Standard CZ builds reach 300 mm web with 3.5 mm material. Beyond that the shaft deflection starts to affect flange squareness and we move to a cassette design with a heavier frame.
Holes are punched in-line by a servo positioned 3-side press that reads the cut length encoder. Change the pattern on the HMI rather than changing tooling, as long as hole sizes stay the same.
Coil width follows the developed length of the section, typically 300–800 mm for purlin. Because web height is adjustable, the line is usually specified with the widest coil it will run and the strip is trimmed or the width set per order.
Next step
Send the profile drawing, material thickness and target output. You will get a line configuration, tooling scope and delivery schedule — usually within one working day.
Or compare non-standard builds on the custom roll forming page.