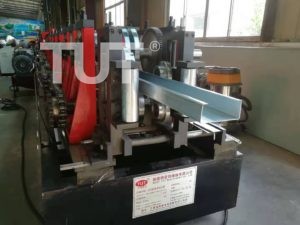
C Purlin Roll Forming Machine
C purlin roll forming machines producing C and U channel sections from 1.5–5.0 mm steel, with in-line punching and hydraulic cutting. Factory direct.
View DetailsPurlin lines
Dedicated lines for C section purlins in 1.5–5.0 mm steel, with adjustable web height, in-line punching and a hydraulic post-cut sized for the section.
C purlin roll forming machines producing C and U channel sections from 1.5–5.0 mm steel, with in-line punching and hydraulic cutting. Factory direct.
View DetailsTechnical overview
Without the switching device a C purlin line has fewer moving parts at the entry, so the strip path is straighter and the line runs faster on the same motor rating.
The section is formed from 1.5–5.0 mm coil in 18–24 stations, with the web height adjustable on the side units and the flange width set by the roll tooling. Lip height and lip angle are the two dimensions buyers check at goods-in, because they control how the purlin sits on the rafter and how the roof sheet fastens.
Punching handles flange holes for the roof sheet, web holes for the sleeve bolts and, on request, service holes for cable. Cutting is a hydraulic post-cut with a shear blade shaped to the section, so the C does not collapse at the cut. If your order book also carries Z purlin, compare with the CZ purlin line before deciding.
Figures are typical for this category. Final values follow the profile drawing and material grade.
Discuss your specificationApplications
The same machine serves different industries depending on the profile, coating and output. Start from the application closest to your project.
FAQ
Answers come from real quotation discussions. If your question is not here, ask it directly and an engineer will answer.
The C line forms a channel with two parallel flanges. The Z line forms a section whose flanges point in opposite directions, so Z purlins nest and lap at the supports. The frames are similar; the tooling and the entry guide differ.
Yes, within the design range — normally 80–350 mm. The side forming units move on linear guides and the shaft line stays in mesh, so height change takes 30–60 minutes.
Weight and container count follow the station count, the shaft size and the scope of supply, and both are confirmed on the shipping plan once the configuration is fixed. The forming bed splits into bolted sections so it can be packed and handled at the destination.
Coil from 1.5 mm up to 5.0 mm on this frame, with the upper limit set by the section geometry and confirmed against your drawing at the order stage. Above that we quote a heavier frame rather than stretch this one.
Next step
Send the profile drawing, material thickness and target output. You will get a line configuration, tooling scope and delivery schedule — usually within one working day.
Or compare non-standard builds on the custom roll forming page.