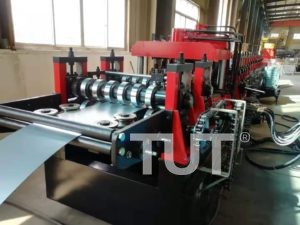
CZ Purlin Roll Forming Machine
C Z Purlin Roll Forming Machine is used to produce C Purlin and Z Purlins with very less changeover time that the exchange time…
View DetailsPurlin lines
One frame, both sections: C and Z purlins from 1.5–5.0 mm steel, switching between hands and profiles without changing the roll set.
C Z Purlin Roll Forming Machine is used to produce C Purlin and Z Purlins with very less changeover time that the exchange time…
View DetailsTechnical overview
The switching device sits between the decoiler and the first forming pass. It turns the strip through 180 degrees and offsets it, so the same roll train sees either a C or a Z developed width without touching the tooling.
On the C run the strip feeds straight into the forming bed. On the Z run the entry guide flips the strip so the flanges form in opposite directions. Switching section hand is about one minute — it is the web height change that takes 20–40 minutes with two technicians, including the reset and a trial length check. That second figure is the one that matters commercially, because it decides whether small mixed orders are worth taking.
The frame runs 20–24 stations on 80 mm shafts with a 15 kW main motor, and in-line 3-side punching that follows the cut length by servo. Because both hands of Z alternate at each rafter, the line is normally set up to run left and right hand Z back to back. See the purlin overview to compare the three builds.
Figures are typical for this category. Final values follow the profile drawing and material grade.
Discuss your specificationApplications
The same machine serves different industries depending on the profile, coating and output. Start from the application closest to your project.
FAQ
Answers come from real quotation discussions. If your question is not here, ask it directly and an engineer will answer.
Two different numbers, often confused. Switching the section hand is about one minute, because the entry guide flips the strip and no tooling is touched. Changing web height is the slow part: 20–40 minutes for two technicians, measured from last C cut to first saleable Z length, including the reset and a trial length check.
The guide uses nylon-faced rollers and a controlled side load, so prepainted and galvanized surfaces are not scored. Customers inspecting first-off samples usually cannot identify the switch side.
No. Height is set with the line stopped and the side units locked mechanically. Adjustment on the move is possible on cassette designs but not on this frame.
If the web height does not change, switching section takes about a minute and almost any order size is worth running. Once the web height has to be reset, allow 20–40 minutes, so batching several small orders of the same web height is more efficient than switching repeatedly.
Next step
Send the profile drawing, material thickness and target output. You will get a line configuration, tooling scope and delivery schedule — usually within one working day.
Or compare non-standard builds on the custom roll forming page.